Custom OEM Health Informatics Solutions Supplier & Suppliers

Architecting Next-Generation Connected Medical Hardware, Telemetry Nodes & Enterprise Interoperability Systems for Global Healthcare Providers

Featured OEM Medical Hardware & Informatics Products

Explore our ISO 13485 certified medical devices, diagnostic platforms, and integration-ready healthcare hardware built for global OEM distribution.

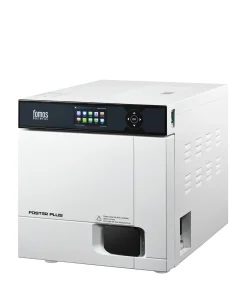
Advanced Ethylene Oxide Gas Sterilization for Medical Equipment
View Specifications
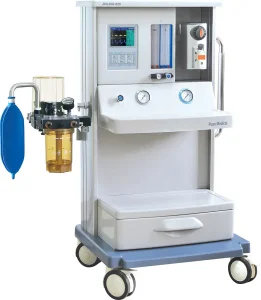
Factory Supply Medical Equipment Anesthesia System of ICU & Emergency Hospital Ventilator
View Specifications
Laboratory Gc Machine Gas Chromatography Instrument Gas Chromatography Device
View Specifications
Ot-6b Hospital Legs Orthopedics Traction Device for Operating Room Equipment
View Specifications
Od1-Ap Eyes Diagnostic Equipment with Internal Thermal Printer and Touch Monitor
View Specifications
Anesthesia System of ICU & Emergency Jinling 01 Factory Supply Hospital Ventilator Medical Equipment
View Specifications
Sleep Apnea Therapeutic Device (THR-PV01)
View Specifications
Shanghai Control Brother Medical or Your Brand Beside Hospital Furniture
View Specifications

Pioneering Custom OEM Health Informatics Hardware & Ecosystem Integration

In the contemporary digital healthcare landscape, the convergence of clinical medical hardware and intelligent health informatics solutions forms the backbone of modern clinical workflows. Modern healthcare institutions no longer demand isolated medical instruments; they require fully integrated, interoperable, and secure medical hardware ecosystems capable of transmitting zero-latency clinical telemetry directly into Electronic Health Record (EHR) systems via standardized HL7 FHIR and DICOM protocols.

As a premiere Custom OEM Health Informatics Solutions Supplier, Qingdao MDV Medical Appliances Co., Ltd. stands at the forefront of this industrial transformation. We bridge the critical gap between high-precision physical manufacturing—encompassing anesthetic systems, ICU ventilation devices, diagnostic instrumentation, and point-of-care telemetry hubs—and scalable digital health architectures.

Information Gain Architecture: Our OEM/ODM frameworks do not merely manufacture hardware; we integrate edge-computing firmware, biometric data encryption modules, and automated remote monitoring protocols that lower Total Cost of Ownership (TCO) while upholding strict FDA 510(k), CE MDR, and ISO 13485 compliance standards.

Core Engineering Pillars

  • Interoperable Hardware Integration: Native support for HL7, DICOM, and MQTT IoT data transport layers.
  • ISO 13485 Certified Manufacturing: Advanced 1,500 m² cleanrooms guaranteeing clinical sterility.
  • Custom Firmware & White-Labeling: Turnkey UI/UX, embedded algorithms, and regionalized language packs.
  • Cybersecurity Compliance: End-to-end AES-256 data encryption aligned with HIPAA & EU GDPR.
6,600 m²
Total Enterprise Footprint
1,500 m²
ISO-Class Cleanroom Facilities
50+
Specialized R&D & QA Engineers
ISO 13485
Certified Quality System & CE

The Spectrum of Custom OEM Health Informatics Hardware

Delivering integrated hardware solutions customized to your brand’s technical parameters, operational demands, and regional medical certifications.

ICU & Ventilator Informatics Telemetry

Our critical care platforms, such as the ICU Emergency Hospital Ventilator and Anesthesia Systems, are embedded with custom sensor arrays and digital interfaces. They stream real-time physiological metrics—including peak airway pressure, minute volume, and oxygen saturation—directly into central hospital command centers, ensuring critical telemetry is archived without manual entry errors.

Remote Patient Monitoring (RPM) Nodes

To support decentralized healthcare and telehealth initiatives, we offer white-label portable devices like the Cbmcare Remote Health Monitoring Device and Aerti Portable Healthcare Oxygen Systems. Built with low-power cellular (NB-IoT/LTE-M) and Bluetooth Low Energy (BLE) modules, these units collect biometric trends at home and securely transmit them to cloud-based diagnostic portals.

Diagnostic & Laboratory Informatics Devices

From Gas Chromatography (GC) devices to internal thermal printer-integrated Ophthalmic Diagnostic Equipment and Refurbished Biotek ELISA Readers, our diagnostic hardware is engineered with integrated RS232, USB, and LAN communication ports for instant LIMS (Laboratory Information Management System) sync.

Global Regulatory Compliance & Localized Governance

Navigating complex international medical device frameworks with validated compliance, rigorous quality assurance, and localized market adaptability.

Medical Class Certification

Our manufacturing plant in Qingdao is certified under ISO 13485 Medical Device Quality Systems. Select product lines carry European CE Certification under the Medical Device Regulation (MDR EU 2017/745), ensuring smooth regulatory filing across global jurisdictions including North America, LATAM, EMEA, and SEA.

Data Privacy & Cybersecurity

Health informatics solutions demand robust data protection. Our firmware engineering adheres to HIPAA standards in the United States and GDPR data sovereignty guidelines in Europe. Embedded systems feature hardware-level encryption (TPM 2.0 modules) and encrypted data transmission to safeguard patient health information (PHI).

Localized UI/UX & Support

We support multi-language touch monitor interfaces, regionalized power specs (110V/220V, 50/60Hz), custom alarm protocols according to local clinical habits, and modular power supplies to comply with localized electromechanical safety norms (IEC 60601-1).

The Qingdao MDV Supply Chain Advantage: Infrastructure & Production Rigor

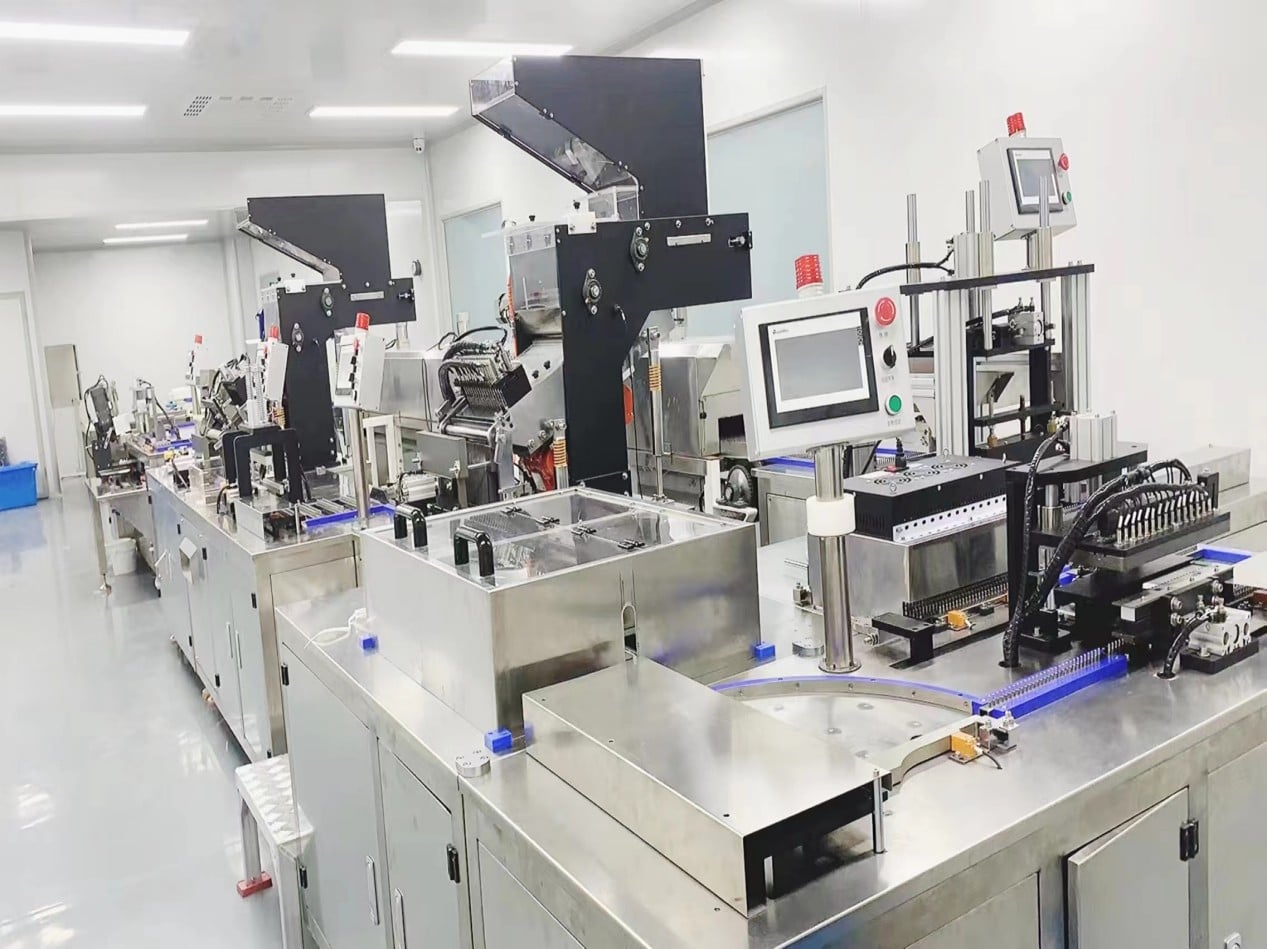
Partnering with an established Chinese OEM manufacturer provides global healthcare distributors, hospital networks, and medical brand owners with unmatched cost efficiency, scale, and engineering agility. Qingdao MDV Medical Appliances Co., Ltd. operates a sophisticated 6,600 square meter enterprise campus, meticulously divided to maintain international standards of sterility, micro-contamination control, and electronic precision.

Controlled Production Cleanrooms

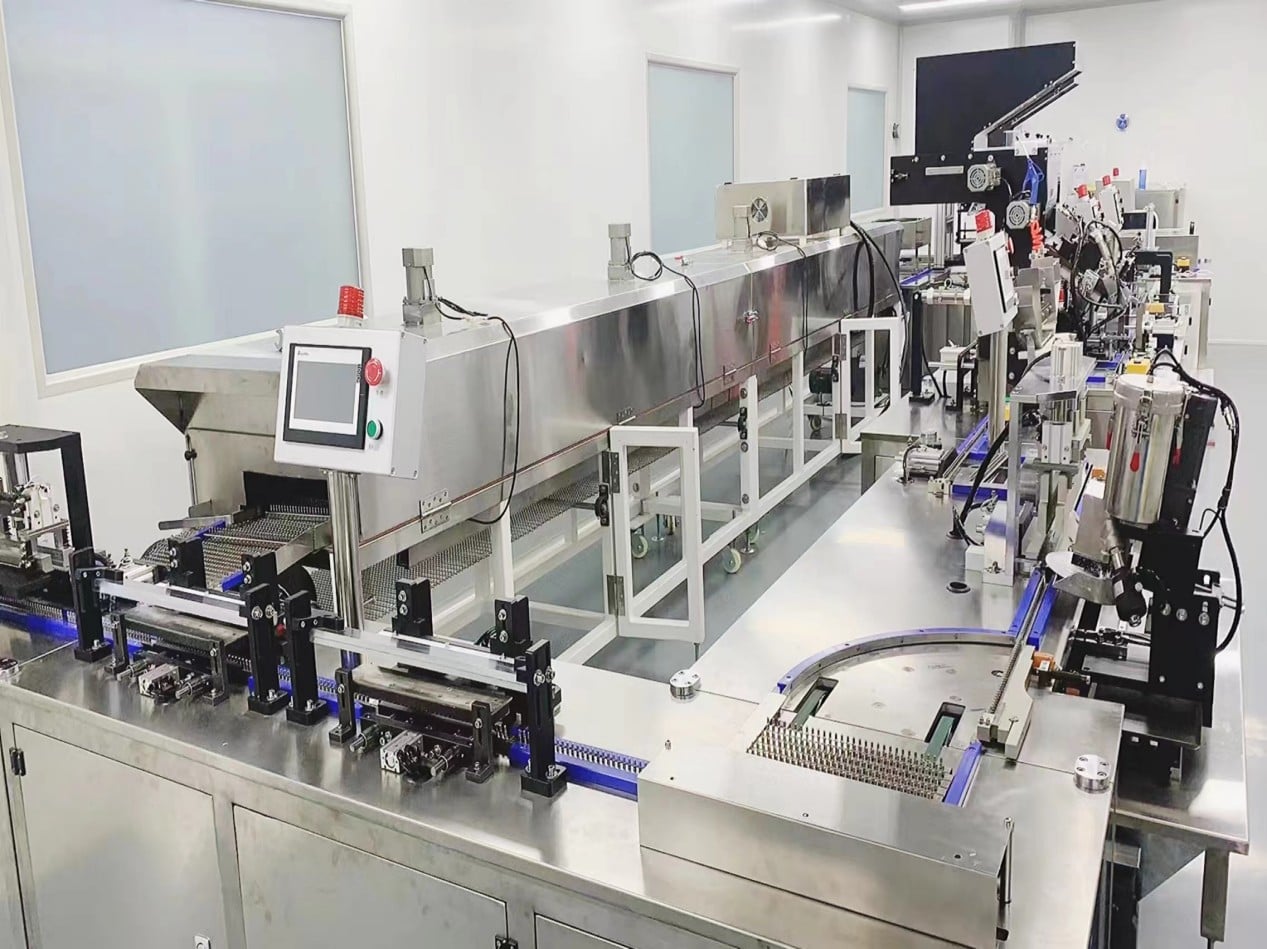
Our facility houses a 1,500 sqm ISO Class 8 (100,000-grade) Cleanroom dedicated to high-precision assembly of anesthetic circuits, puncture needles, respiratory valves, and interventional tubing, preventing particulate contamination before final sterilization.

Dedicated Quality Inspection Zone

A specialized 200 sqm QA/QC Testing Center equipped with advanced spectrum analyzers, automated calibration rigs, and pneumatic leak detectors to evaluate every single ventilator, monitor, and sterilization unit prior to factory acceptance testing (FAT).

End-to-End Sterilization & Processing

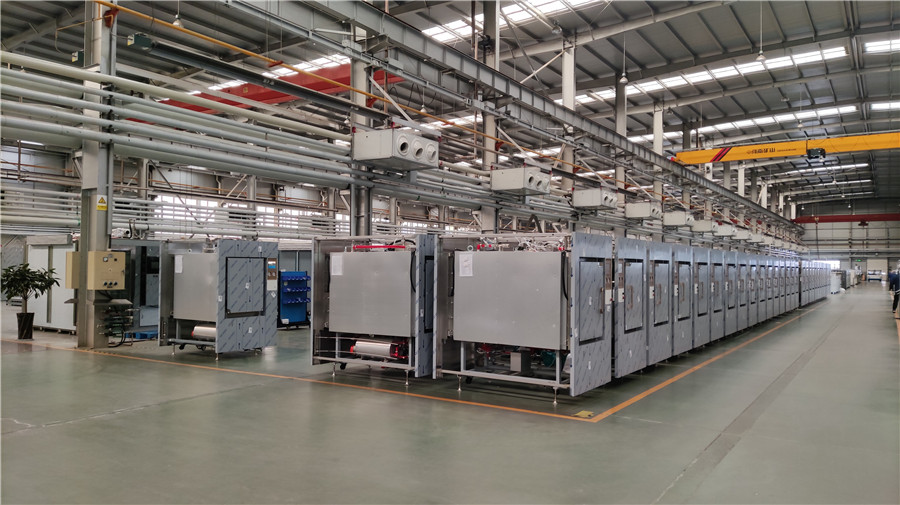
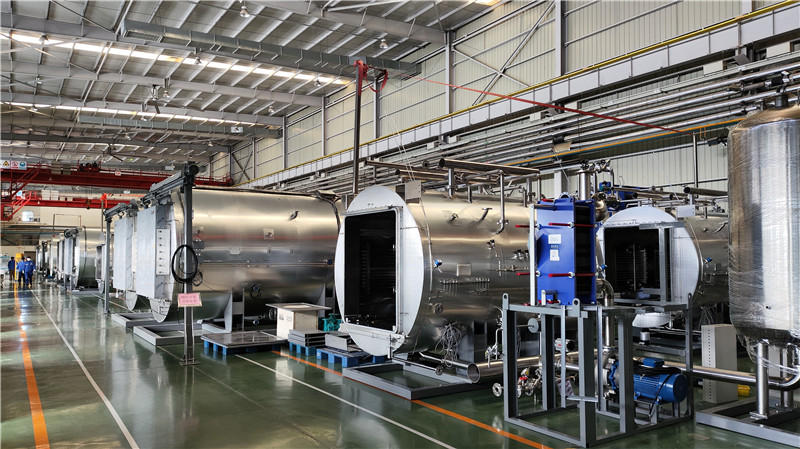
We feature integrated Ethylene Oxide (EtO) Gas Sterilization Chambers and automated microwave-steam waste treatment systems, enabling seamless batch processing, bio-burden validation, and turnkey OEM packaging under pristine conditions.
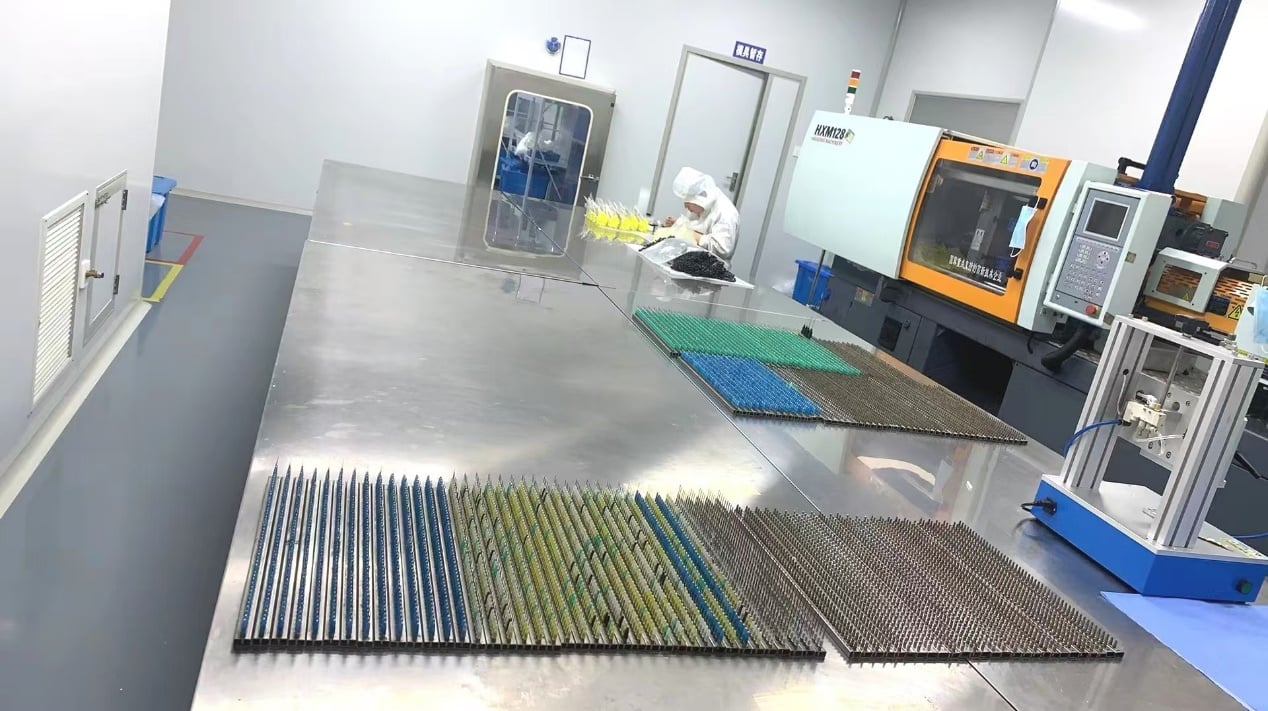
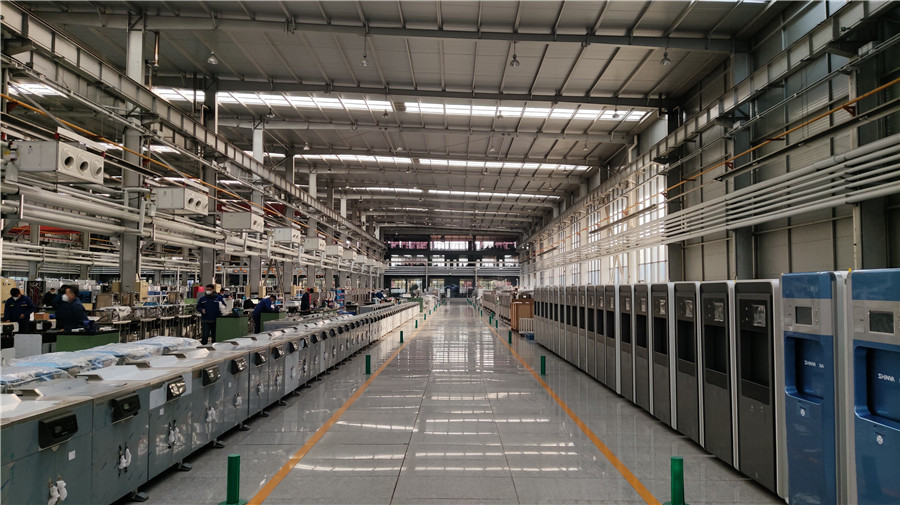
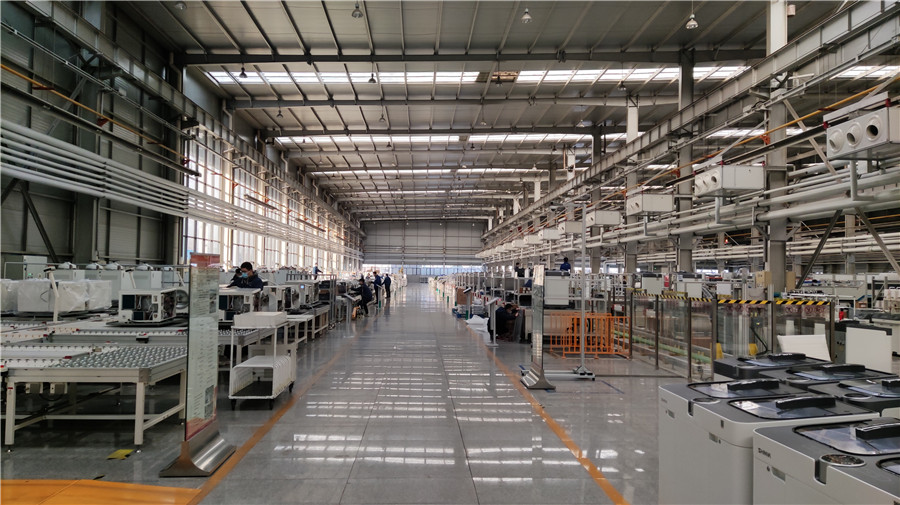
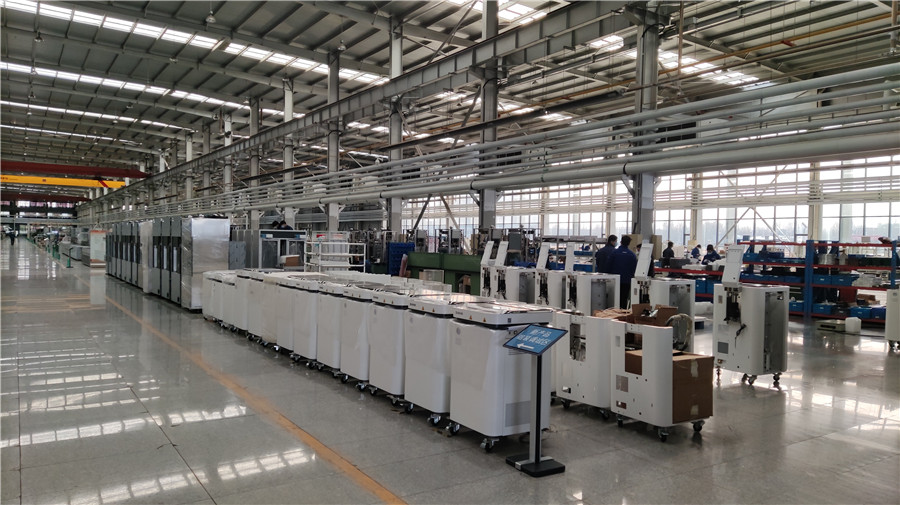
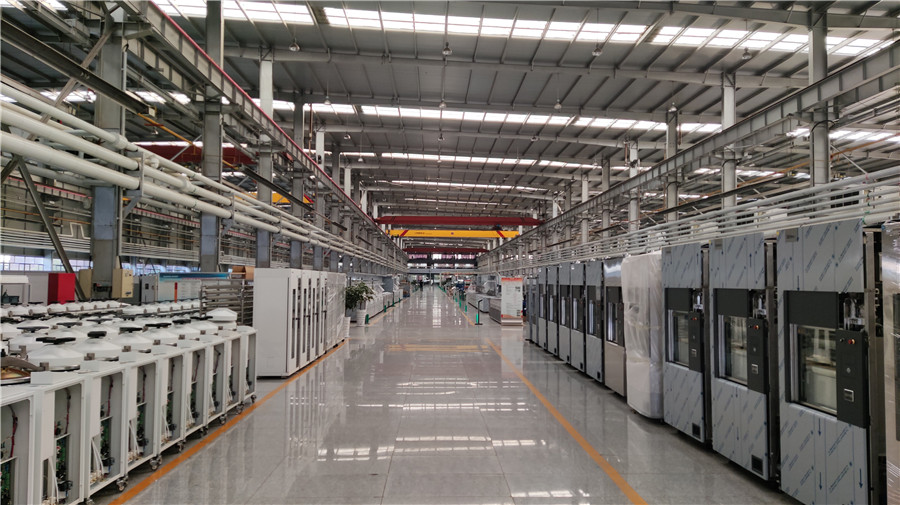
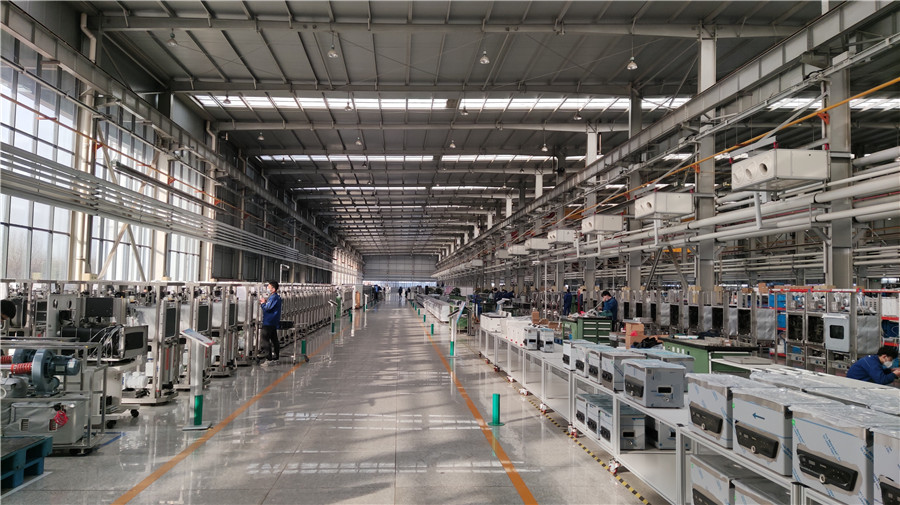
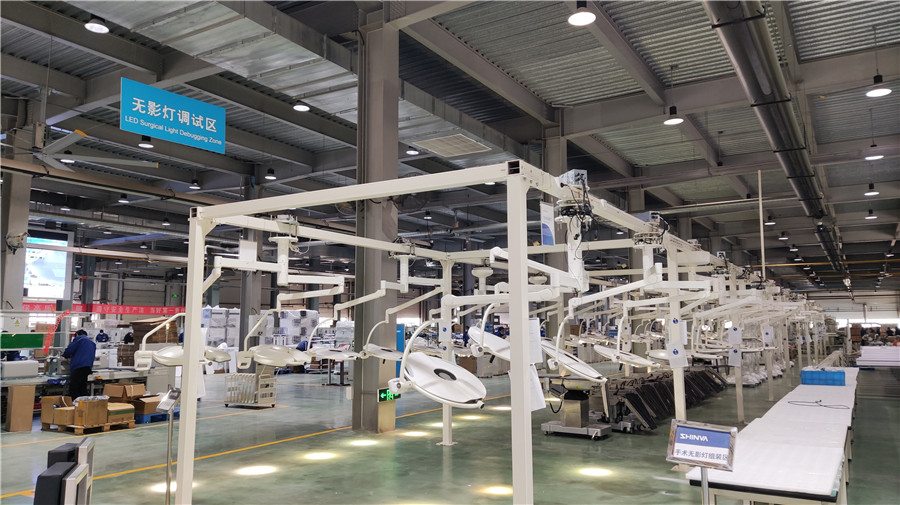
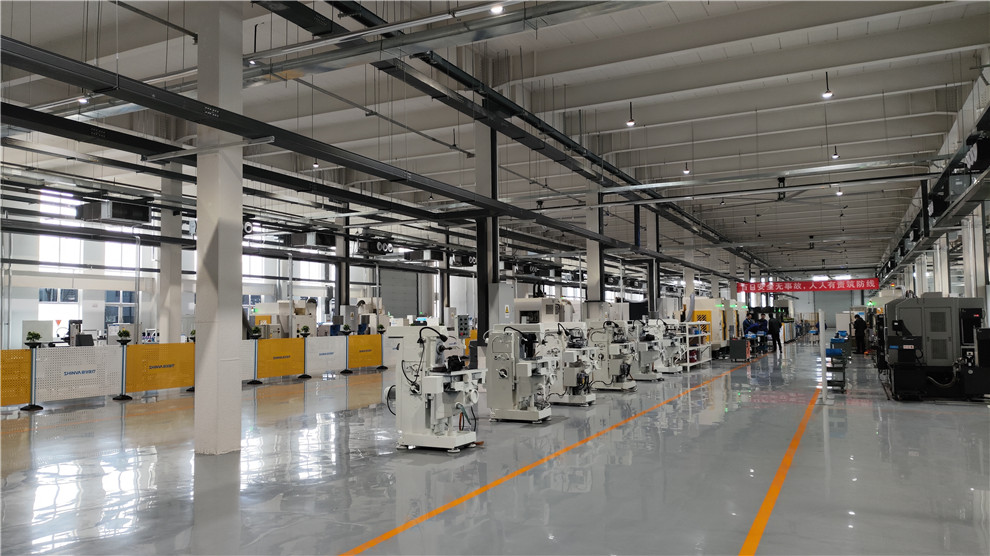
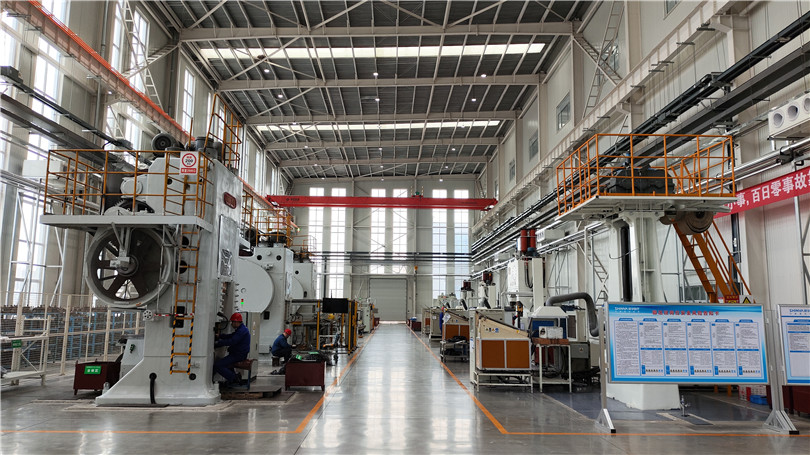
Qingdao MDV Factory Floor & Cleanroom Facilities

Strategic Global Procurement: Optimizing TCO for Medical Equipment

Healthcare system procurement directors, B2B importers, and original brand manufacturers face persistent pressure to reduce Total Cost of Ownership (TCO) without compromising patient safety or data integrity. Our custom OEM health informatics framework is structured to streamline every phase of the procurement life cycle:

1. Bill of Materials (BOM) Optimization

Leveraging localized component sourcing in China’s medical manufacturing clusters allows us to lower direct hardware BOM costs by 25% to 40% compared to Western counterparts, preserving capital for software R&D.

2. Rapid Turnkey Prototyping

From initial CAD modeling and firmware flash testing to functional 3D prototypes, our 50-person specialized team accelerates time-to-market (TTM) for original brand launches by up to 50%.

3. Scalable Minimum Order Quantities (MOQs)

We offer flexible contract terms designed for growing healthtech companies as well as high-volume institutional hospital tenders, supporting small-batch validation runs up to mass containerized shipments.

4. Complete Life Cycle Logistics & Support

Our comprehensive export logistics include climate-controlled packaging, full customs documentation, spare parts supply chains, and multi-year technical maintenance warranties.

Emerging Industry Trends in Connected Healthcare & Informatics

Staying ahead of technological shifts to build futuristic, high-gain medical hardware ecosystems.

Edge AI & Predictive Clinical Analytics

Modern intensive care environments are moving away from passive monitoring toward predictive alert systems. Intelligent OEM hardware now incorporates microcontrollers capable of running lightweight AI models directly at the bedside, recognizing subtle patterns of hemodynamic instability, respiratory distress, or cardiac arrhythmia before overt symptoms manifest.

Software as a Medical Device (SaMD) Fusion

Hardware is increasingly becoming the physical host for advanced software platforms. Our health informatics solutions are engineered with standardized APIS and open SDKs, permitting third-party SaMD developers to deploy proprietary diagnostic algorithms seamlessly across our monitor and diagnostic hardware line.

Sustainable & Eco-Friendly Healthcare Tech

With stringent global ESG mandates, healthcare facilities are prioritizing eco-conscious manufacturing. Qingdao MDV integrates low-power microprocessors, recyclable medical-grade polymers, and energy-efficient microwave waste sterilization technology that minimizes environmental impact while maintaining hospital-grade performance.

Clinical Application Scenarios Across the Healthcare Continuum

Our OEM health informatics hardware and specialized medical products are designed for seamless integration across diverse clinical environments, optimizing staff workflow, patient safety, and centralized data management.

Operating Theater & Anesthesia Control

Integrated anesthesia delivery workstations synced with precision traction devices and gas chromatography monitoring, enabling surgical teams to monitor real-time gas exchange, volatile agent delivery, and biomechanical parameters from a single interface.

ICU & Critical Care Telemetry

Continuous ventilation monitoring, invasive blood pressure telemetry, and automated oxygen therapy management integrated directly into hospital EHR systems for 24/7 patient surveillance.

Outpatient, Home Health & Telehealth Nodes

Compact remote health monitoring stations, portable travel oxygen concentrators, and sleep apnea therapy systems equipped with cellular gateways for automated remote care management.
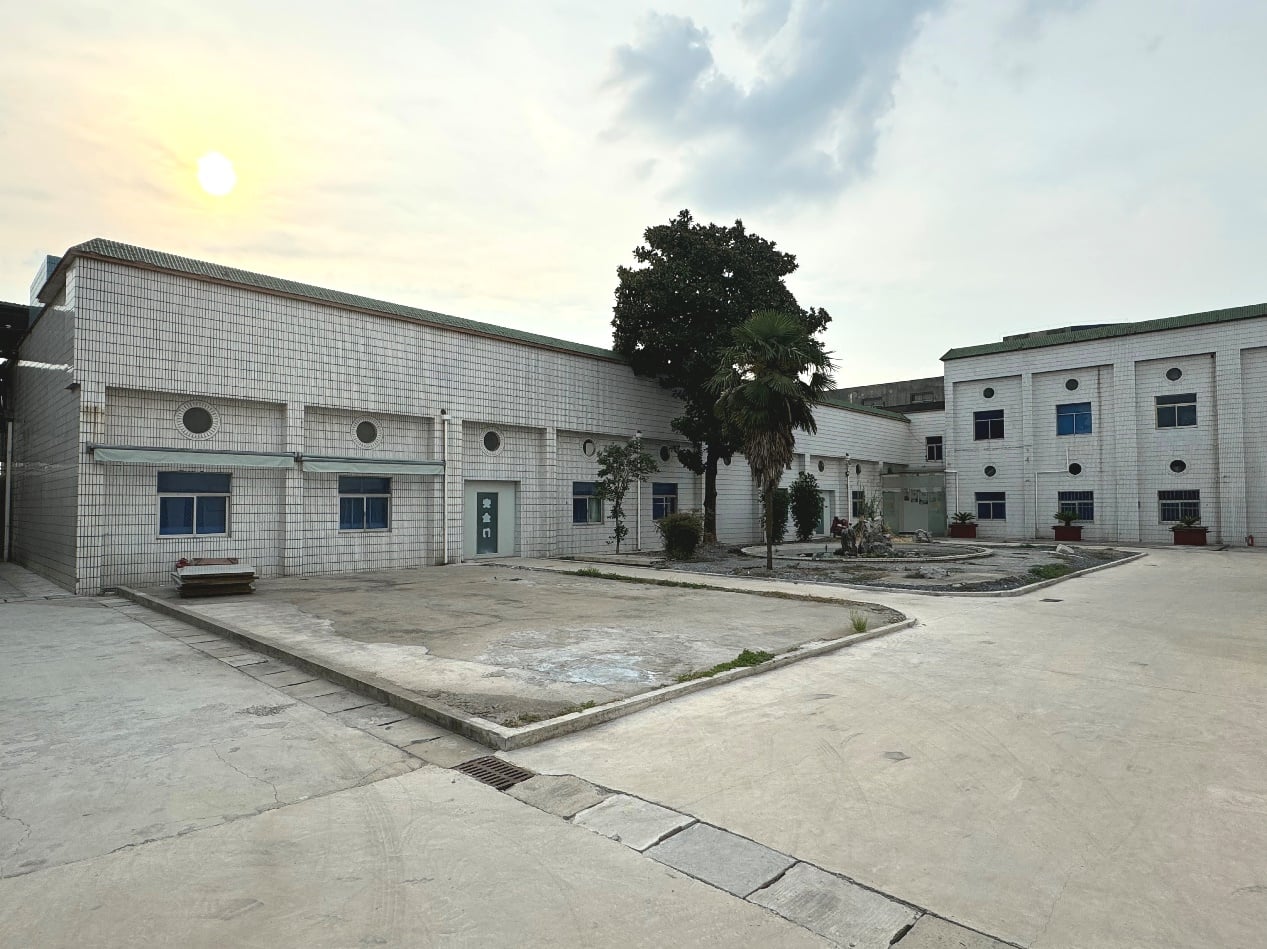
Facility & Application Gallery

Frequently Asked Questions (FAQ) & Technical Insights

Detailed answers addressing procurement criteria, technical standards, regulatory compliance, and OEM customization capabilities.

What communication protocols do your health informatics hardware platforms support for hospital system integration?
Our connected medical hardware supports a wide spectrum of standardized healthcare messaging protocols. Built-in interfaces feature native support for HL7 v2.x/v3.0 and HL7 FHIR standards for Electronic Health Record (EHR) synchronization. For imaging systems (such as MRI and diagnostic monitors), we maintain full DICOM 3.0 compliance. Remote and home health telemetry devices utilize low-bandwidth, secure MQTT and HTTPS protocols over Wi-Fi, Ethernet, BLE 5.0, or cellular NB-IoT/LTE-M networks.
How does Qingdao MDV handle Intellectual Property (IP) security during custom OEM contract manufacturing?
We prioritize absolute IP protection for all enterprise OEM/ODM partners. We establish formal, legally binding non-disclosure agreements (NDAs) prior to any engineering disclosures. Proprietary firmware source code, circuit schematics, and mechanical molds remain the exclusive property of the client. Furthermore, our production cleanrooms and firmware flashing lines operate on isolated networks to prevent unauthorized data access or software leaks.
What quality management certifications govern your manufacturing processes?
Qingdao MDV Medical Appliances Co., Ltd. operates strictly under ISO 13485:2016 Medical Device Quality Management System standards. Our facilities undergo annual audits by accredited notified bodies to verify compliance with cleanroom cleanliness standards (ISO Class 8 / 100,000-grade), risk management (ISO 14971), and electromechanical safety (IEC 60601-1). Product lines destined for international markets carry CE marks aligned with EU MDR guidelines.
What level of physical and graphical customization is offered for OEM branding?
We provide full-spectrum OEM white-label customization. This includes custom plastic injection molding chassis colors, silk-screened brand logos, custom packaging, localized power cables, custom user interface (UI) graphical skins, multi-language system firmware, and custom user manuals. We also tailor internal hardware components (e.g., specific sensor modules or communication chips) to meet specific target performance specs.
How does your factory ensure the safety and efficacy of sterile equipment like EtO sterilizers and respiratory tubing?
Sterile medical equipment undergoes rigorous microbiological and chemical testing. Our Ethylene Oxide (EtO) sterilization processes are validated per ISO 11135 standards. We perform biological indicator testing, residual EtO gas analysis via gas chromatography (GC), and sterile barrier integrity testing for every production batch before granting Quality Assurance release.
What is the typical lead time from prototype design to full mass production?
Standard OEM production lead times depend on project complexity. For catalog-standard hardware with simple branding modifications, production typically takes 3 to 4 weeks. For complete custom ODM engineering (requiring new tooling molds, customized PCBAs, and software integration), prototype samples are delivered within 60 days, followed by regulatory validation and full-scale mass manufacturing within 90 to 120 days.

Complete Healthcare Equipment & Systems Catalog

Explore our extended portfolio of respiratory care systems, diagnostic instrumentation, remote monitors, and hospital infrastructure solutions.
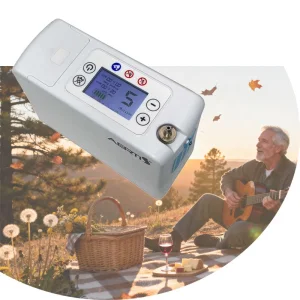
Aerti Elderly Healthcare Oxygen Machine 1L Portable Oxygen Device for Travel
View Specifications
2. Cbmcare Remote Health Monitoring Device with Customized Specifications
View Specifications
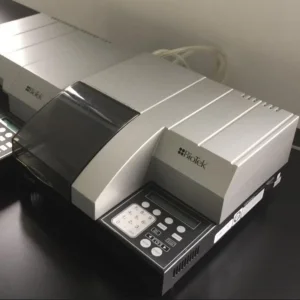
Refurbished Good Condition Lab Biotek Elx800 Elisa Reader Device
View Specifications
CE Eecp-Machine Heart Rehabilitation Equipment with Price
View Specifications
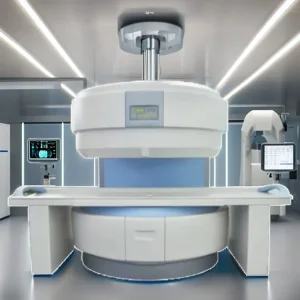
High-Quality MRI Equipment for Medical Diagnostic Imaging
High-Quality MRI Equipment for Medical Imaging and Diagnosis
View Specifications
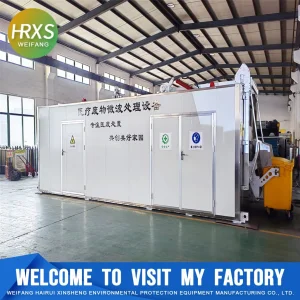
Clinic/Hospital/Healthcare/Lab Using Medical Waste Sterilization Disposal Equipment
Clinic/Hospital/Healthcare/Lab Using Small/Fixed/Mobile Medical Waste Microwave/Steam Sterilization Disposal Equipment
View Specifications
Autoclaves Sterilization Laboratory Equipment High Quality 22L Suitable
View Specifications
Medical Breathing ICU Respiratory Ventilator Respiratory Equipment
View Specifications